Magnetic component manufacturing is rapidly evolving today. We are moving away from subjective manual quality control toward fully automated inspection. This transition is essential for modern production lines. Defective magnets carry immense business costs in downstream applications. An undetected micro-crack in an electric vehicle (EV) motor can cause catastrophic failure. Similarly, a tiny plating defect on a consumer electronics magnet often leads to field corrosion and product recalls. High-stakes industries simply cannot afford these manufacturing blind spots.
This guide will clearly define how automated optical inspection solves these challenges. We will explore the primary functions of modern inspection equipment. You will discover practical evaluation criteria for selecting the right architecture. We also cover the operational realities of deploying these systems in high-volume production environments. By the end, you will know exactly how to integrate a Magnet AOI machine to secure your product yields.
Key Takeaways
Core Function: A Magnet AOI machine replaces subjective manual checks with high-speed, repeatable optical metrology and surface defect detection.
Critical ROI Driver: Significantly reduces the Cost of Poor Quality (COPQ) while maintaining throughput speeds that manual inspection cannot match.
Evaluation Priority: The best systems balance high-resolution imaging with advanced lighting to overcome the reflective glare of magnet coatings (like Ni-Cu-Ni).
Implementation Reality: Success depends as much on mechanical material handling (preventing highly magnetized parts from jamming or attracting) as it does on camera specifications.
The Primary Functions of a Magnet AOI Machine
Manufacturers rely on automated inspection to guarantee component integrity. You cannot build reliable motors or sensors using flawed magnetic materials. A Magnet AOI machine performs several distinct functions simultaneously. It evaluates every single part passing down the line. We can categorize these functions into three main areas of operation.
Surface Defect Detection (Yield Protection)
Magnets are inherently fragile. Materials like sintered NdFeB or Ferrite chip very easily during handling. An optical inspection system constantly scans these fragile surfaces. It looks for various structural and cosmetic flaws. You can rely on the equipment to spot microscopic issues before they leave your facility.
It identifies chips, micro-cracks, scratches, and pinholes on the magnet surface.
It catches these physical deformities before parts undergo final magnetization.
It detects coating and plating anomalies like blisters or oxidation.
It flags uneven plating layers before they lead to severe field corrosion.
Surface integrity directly impacts long-term reliability. A tiny pinhole in a nickel coating lets moisture reach the neodymium core. The magnet will oxidize and expand over time. This expansion destroys the surrounding assembly. Automated inspection prevents this specific failure mode entirely.
High-Precision Dimensional Metrology
Modern assemblies require tight geometric tolerances. You must ensure every component fits perfectly into the final product. A Magnet AOI machine measures physical dimensions with extreme accuracy. It uses high-resolution cameras to verify these measurements in real time.
It verifies geometric tolerances such as length, width, and thickness.
It checks concentricity against strict engineering specifications.
It ensures chamfer and radius uniformity across every batch.
Uniform chamfers are absolutely critical for automated motor assembly lines. Robotic arms cannot insert magnets into tight stator slots if the edges are jagged. The optical system measures these tiny edge angles instantly. It rejects any part falling outside your specified tolerance window.
Orientation and Polarity Visual Verification
Correct alignment is vital for magnetic performance. Installing a magnet backward ruins the magnetic circuit. Manufacturers often use visual indicators to denote specific poles. An automated system checks these markers flawlessly.
It detects laser markings used to denote magnetic poles.
It verifies the presence and clarity of painted visual indicators.
It flags misaligned or incorrectly oriented magnets prior to final packaging.
It prevents downstream assembly errors caused by reversed polarity.
Human operators easily miss small laser marks during long shifts. The machine never misses them. It confirms the orientation of hundreds of parts per minute. You can ship your products knowing they are configured correctly.
How PTC Magnet Cosmetic Inspection Equipment Applies AOI in Production
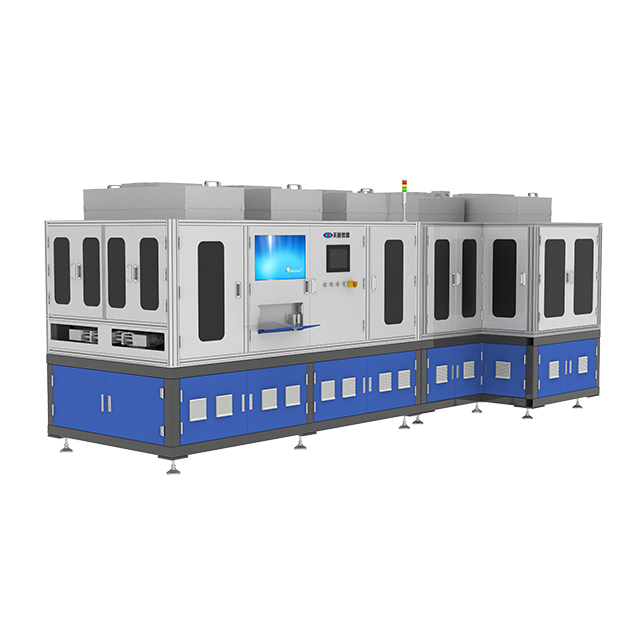
For manufacturers that need to turn these inspection functions into a practical production process, PTC offers dedicated Magnet Cosmetic Inspection Equipment. The system integrates loading, automatic inspection, and unloading so magnet appearance and dimensional checks can be completed in a continuous workflow rather than as a separate manual inspection step.
The equipment is designed to inspect both product dimensions and common cosmetic defects, including pinholes, bumps, notches, stripes, cracks, bright spots, and stains. After inspection, the system automatically determines whether each product is OK or NG and sorts the parts accordingly. Defect categories, sizes, and location coordinates can be displayed and recorded together with the original inspection images, supporting re-inspection and production analysis.
AI-assisted defect recognition: The software can automatically mark defects, support model training, and filter false defects to improve inspection consistency and product yield.
Production data management: Inspection data can be queried, exported, and analyzed, while the system can also connect with MES for production monitoring and traceability.
Automated sorting: OK and NG products are identified automatically and directed to the corresponding bins, reducing the dependence on manual sorting.
High-throughput inspection: The specified inspection efficiency is about 2,100 pcs/h, with an inspection rate of 99.9% and an overkill rate of no more than 1% under the stated product specification.
This type of system is especially relevant to high-volume 3C manufacturing environments where cosmetic consistency, dimensional control, and traceable quality data are required at the same time. You can also explore our broader 3C Equipment range for related automated inspection and handling solutions.
Business Problem Framing: Why Manual Inspection Fails at Scale
Scaling up production exposes the severe flaws in manual quality control. Human beings cannot sustain high-speed visual inspection indefinitely. You will encounter major bottlenecks when relying on human eyes. The physical and cognitive limits of human operators create massive operational risks.
The Limits of Human Vision on Reflective Surfaces
Inspectors face immense difficulty when evaluating highly reflective metallic coatings. Magnets often feature a shiny Ni-Cu-Ni plating. This finish reflects factory lighting directly into the operator's eyes. The resulting glare causes severe visual fatigue.
Operators struggle to distinguish between a harmless surface texture and a critical micro-crack. This ambiguity leads to terrible accuracy metrics. You will see high false-positive rates where good parts are discarded. Worse, you will experience high false-negative rates where defective parts ship to customers. Human vision simply cannot process shiny, tiny details reliably over an eight-hour shift.
Throughput vs. Accuracy Trade-off
Manual inspection fundamentally bottlenecks production speeds. You measure factory output in parts per minute (PPM). Fast production requires fast inspection. Human operators must choose between speed and accuracy. They cannot maximize both.
If you ask operators to work faster, their accuracy drops dramatically. If you demand perfect accuracy, your throughput plummets. A Magnet AOI machine breaks this compromise. It standardizes the cycle time permanently. The system processes thousands of units per hour without fatigue. It maintains perfect consistency regardless of the time of day.
Data Silos and Traceability
Manual sorting leaves no verifiable digital trail. Operators toss parts into "good" or "bad" bins. You never learn why a specific part failed. This creates massive data silos on your factory floor. You cannot improve your process without actionable data.
Automated optical systems solve this tracking problem. They integrate directly with your Manufacturing Execution Systems (MES). The machine provides real-time defect data for every single part. You can trace a cracked magnet back to an upstream slicing issue. You can link blistered coatings directly to a specific plating bath. This traceability enables true root-cause analysis.
Solution Categories: Choosing the Right AOI Architecture
You must select the correct architecture for your specific production environment. Not all optical inspection systems operate the same way. We categorize these solutions based on their imaging technology and their physical placement on the factory floor.
2D vs. 3D AOI Systems
Camera technology defines the system's analytical capabilities. You must choose between two-dimensional and three-dimensional imaging.
2D AOI: This technology is optimal for flat surfaces. It excels at scratch detection and rapid dimensional checks. It operates extremely fast and requires less computing power. It is generally more cost-effective. However, it remains limited on depth analysis. It cannot easily measure the precise depth of a chip.
3D AOI: This technology captures exact topographical data. It is completely necessary for volumetric defect analysis. You need it to measure the exact depth of a surface chip. It also inspects complex, multi-angled magnet shapes perfectly. For example, you must use 3D systems for arc magnets used in EV rotors.
Inline vs. Offline / Standalone Configurations
Physical placement determines how the machine interacts with your existing workflows. You can install systems directly into the line or use them separately.
Inline Systems: We integrate these directly into the conveyor system. They sit post-plating or post-magnetization. They evaluate parts automatically as they flow between stations. This configuration is best for high-volume, continuous manufacturing. It requires zero manual handling.
Offline Systems: These are batch-based testing stations. Operators manually load a tray of parts into the machine. This setup is better for low-volume, high-mix production. It is also ideal for auditing specific batches. Highly regulated buyers in aerospace or medical fields often require these offline validation audits.
Architecture Comparison Chart
System Category
Ideal Application Scenarios
Core Technical Advantages
Primary Limitations
2D Inspection
Block magnets, flat surfaces, fast sorting
High throughput, lower computational load
Cannot measure volumetric depth
3D Inspection
Arc magnets, rotor assemblies, complex geometry
Precise depth measurement, volumetric analysis
Slower processing speed, higher data storage
Inline Setup
Continuous 24/7 manufacturing operations
Zero manual handling, real-time MES data
Requires complex integration into conveyors
Offline Setup
High-mix production, batch auditing, sampling
Flexible changeovers, simple deployment
Requires operators to load and unload trays
Key Evaluation Dimensions for Procurement
Purchasing automated inspection equipment requires careful evaluation. You must look past basic camera megapixels. The best systems integrate specialized hardware and intelligent software. You should assess four critical dimensions before making a procurement decision.
Lighting and Optical Architecture
Lighting is the most important hardware component in optical inspection. You must evaluate the system's ability to manipulate light. The machine must eliminate glare from reflective magnetic coatings entirely.
Look for multi-angle, multi-spectrum lighting arrays. The system should utilize coaxial lighting to highlight flat surfaces. It should use ring lighting to expose raised edges. Low-angle illumination is critical for revealing shallow scratches. By combining these lighting techniques, the cameras capture flawless images without blinding reflections.
Software and AI Capabilities
Software determines how accurately the machine interprets the images. Legacy rule-based software struggles with natural material variations. You should look for deep learning and AI-driven defect classification.
Advanced AI models reduce "false calls" drastically. A false call happens when the machine rejects a perfectly good part. The AI learns the subtle difference between acceptable surface texture and actual micro-cracks. It mimics human judgment but applies it with mathematical consistency. This capability keeps your yield rates high while blocking genuine defects.
Specialized Material Handling
Magnets present unique mechanical challenges for automation. Typical material handling systems often destroy magnetic components. You must scrutinize the internal mechanical design of the machine.
First, the machine must handle brittle materials gently. It cannot induce chips while flipping or routing the parts. Second, it must manage highly magnetized parts safely. Magnets will stick violently to standard metal tracks. The internal conveyors must use non-magnetic materials like specialized plastics or non-ferrous alloys. This prevents parts from jamming the machinery.
Throughput Capability (UPH)
The inspection system must keep pace with your upstream processes. You measure this in Units Per Hour (UPH). Match the machine's processing speed to your current and projected manufacturing line speeds. If your line produces 5,000 units per hour, your inspection system must process at least 6,000 to prevent bottlenecks. Always build a buffer into your throughput calculations.
Implementation Realities, Risks, and Rollout
Deploying new automated technology rarely happens overnight. You will face operational realities on the factory floor. Managing these risks proactively ensures a smooth rollout. We must address calibration, maintenance, and custom engineering.
The Calibration Period
Every intelligent system requires an initial tuning phase. You cannot unbox the machine and expect perfect accuracy on day one. AI and rule-based algorithms need extensive data. You must feed them a large dataset of both good and defective samples.
This calibration period stabilizes false reject rates. The machine learns exactly what your specific defects look like. You will run the system alongside manual inspectors initially. You adjust the sensitivity parameters daily. Once the algorithm matures, you can remove the manual safety net confidently.
Magnetic Dust and Optics Maintenance
Factory environments are inherently dirty. Unplated or freshly machined magnets generate fine magnetic dust. This dust floats through the air and clings to surfaces. It poses a massive risk to sensitive optical equipment.
You must ensure robust environmental sealing around the optical lenses. If magnetic dust settles on a camera lens, image quality degrades immediately. The machine will start rejecting good parts. You must establish strict preventative maintenance schedules. Operators should clean the optical enclosures regularly using specialized, non-abrasive techniques.
Vendor Support and Customization
Off-the-shelf solutions rarely work perfectly for specialized magnetic components. Emphasize the importance of selecting a flexible vendor. They must be capable of designing custom feeding mechanisms.
Your specific magnet geometries might require unique bowl feeders. Large rotor magnets might need robotic pick-and-place systems. The vendor must engineer these solutions specifically for your product line. Strong technical support during the integration phase determines your ultimate success.
Standard Implementation Steps
Gather a diverse dataset of both acceptable and defective magnet samples.
Work with the vendor to train the AI algorithms on your specific parts.
Install the custom material handling mechanisms (bowl feeders or conveyors).
Run the machine offline to validate initial false call rates against human inspectors.
Integrate the system fully into the inline production flow.
Connect the machine to your MES for real-time defect tracking and analytics.
Conclusion
The function of a Magnet AOI machine extends far beyond simply finding bad parts. It acts as a comprehensive tool for process control and yield optimization. By replacing subjective manual checks, you establish a reliable, high-speed quality gateway. You protect your downstream customers from catastrophic failures.
Deploying these systems successfully requires careful planning. You must evaluate the optical architecture to ensure it handles reflective coatings. You need AI software capable of minimizing false calls. Furthermore, you must verify that the mechanical handling systems will not damage your fragile components.
Your logical next step is active testing with representative samples. A Proof of Concept (PoC) using your most difficult-to-inspect magnet parts can help verify whether the selected optical configuration, defect criteria, handling method, and software settings are suitable for your actual production conditions. If you are evaluating automated magnet inspection for a new or existing line, contact PTC to discuss your sample requirements, inspection targets, and line integration needs.
FAQ
Q: Can a Magnet AOI machine inspect un-magnetized (blank) magnets?
A: Yes. In fact, inspecting parts before magnetization is often easier for automated handling systems, as it prevents parts from clumping together.
Q: How does AOI handle the reflective glare of Nickel-plated neodymium magnets?
A: High-end systems utilize structured illumination (such as dome lighting or multi-phase strobe lights) combined with polarized filters to neutralize glare and reveal sub-surface defects.
Q: What is a typical false-call rate for an AI-powered AOI system?
A: While legacy rule-based systems might see false-call rates of 5-10% on complex surfaces, properly trained AI systems can typically reduce this to under 1%, minimizing unnecessary manual re-inspection.
 English
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 Bahasa Melayu
 தமிழ்
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 українська
 Suomi
 Հայերեն
 עברית
 Latine
 Shqip
 বাংলা
 Eesti keel
 Oʻzbekcha
 latviešu
 Беларуская мова
 Esperanto